Top Glass Filled PTFE Tube Manufacturer Guide: Properties, Uses, and Selection Tips
2026-11-02
When choosing a glass filled PTFE tube, most guides repeat the same generic list of properties and leave you guessing about real-world performance. This one doesn't. From chemical resistance and dimensional stability to wear behavior under load, we break down what actually matters—and where TAIFNO fits into your sourcing decisions. If you're tired of sifting through vendor claims, here's a practical look at properties, uses, and selection tips that can save you time and costly mistakes.
Where the Glass Actually Goes: Composition and Wear Resistance
Most people assume all glass is the same, but the material on a phone screen, a watch face, or a camera lens has been tuned for its exact spot. High-wear surfaces often use aluminosilicate compositions, where sodium ions are swapped for larger potassium ions near the surface to create compressive stress. That stress makes the glass harder to scratch but also slightly more prone to shattering if dropped at the wrong angle. Sapphire, which is technically a crystalline form of aluminum oxide, sits at the extreme end of scratch resistance and gets reserved for small, thick pieces like watch crystals or fingerprint sensor covers.
Wear resistance isn't just about hardness, though. A glass that resists scratches might chip more easily along its edges, so manufacturers adjust the edge profile and the surrounding frame to absorb impact before the glass does. Testing typically involves dragging diamond-tipped indenters across the surface and measuring the width of the resulting groove; the narrower the groove, the better the wear performance. In real use, pocket sand and keys rarely scratch modern aluminosilicate glass, but a single grain of quartz can still leave a mark if it's pressed hard enough.
The placement of each glass type depends on a balance of cost, optical clarity, and how much abuse that area is expected to take. Front display glass leans toward high ion-exchange depth for drop survival, while rear camera covers often get a thinner layer of the same or a slightly different composition to keep scratches from ruining image quality. Over time, even the toughest glass develops micro-abrasions that scatter light, which is why replacement lenses and screen protectors remain a steady aftermarket category.
When to Choose This Grade Over Unfilled or Carbon-Filled Tube
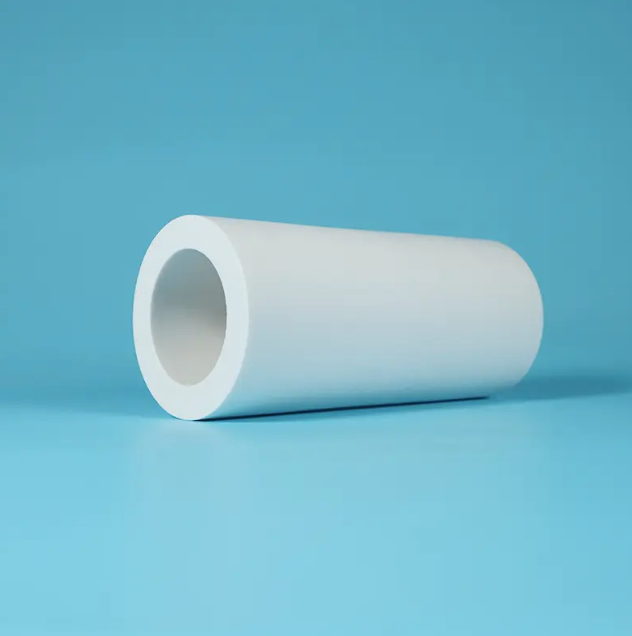
Unfilled tube tends to deform under sustained compressive loads, especially in slow-rotating or oscillating bushings. This grade resists that cold-flow behavior far better because the filler interrupts polymer chain slippage along the load axis. If you have been replacing unfilled bushings due to wall thinning or loss of interference fit, the switch is straightforward.
Carbon-filled tube solves the creep problem and adds static dissipation, but that conductivity is not always desirable. In electrical isolation, cleanroom, or food-contact areas where dark particle shedding is a concern, this grade offers a cleaner option while still improving wear life and dimensional stability over unfilled material. It works particularly well when the assembly runs dry or with minimal lubrication and the mating surface cannot tolerate carbon smearing.
Real-World Uses: From Chemical Processing to High-Load Bearings
When a chemical plant needs to move corrosive fluids at steady pressure, the pump internals often rely on materials that can shrug off both acid and abrasion. Take the impeller shaft in a fertilizer production line: it spins for months on end inside a bath of ammonium phosphate slurry, where ordinary steel would pit and seize within weeks. The solution frequently involves ceramic or carbide sleeves paired with specialized seal faces that resist chemical attack while maintaining a tight clearance. Their performance isn't about a single dramatic event but about surviving countless tiny erosive impacts every minute, which is exactly the kind of unglamorous endurance that keeps a plant running without unscheduled shutdowns.
Shift to a different kind of stress, and you'll find the same design principles hiding inside a giant slew bearing on a dockyard crane. Here the load isn't corrosive; it's overwhelmingly heavy and unevenly distributed. The bearing must rotate smoothly whether the crane is lifting a forty-ton container or swinging empty in a salt-laced sea breeze. Engineers often specify induction-hardened raceways and carefully matched rolling elements, allowing the bearing to spread the load across dozens of contact points instead of a few. It's a quiet compromise between hardness and toughness: hard enough to resist flattening under peak load, tough enough not to crack when a gust of wind jerks the boom mid-swing.
Between these extremes lie a dozen other niches where the same material and geometry decisions quietly determine whether a machine lasts five years or fifteen. Paper mill rollers coated with tungsten carbide shrug off abrasive cellulose fibers while running at high speed. Wind turbine pitch bearings operate in stop-start motion, never completing a full revolution, yet they must withstand both storm gusts and constant micro-movements. In each case, the real-world use isn't a single impressive spec sheet number; it's the accumulation of small design choices that keep something heavy, corrosive, or awkwardly loaded moving reliably long after the warranty expires.
What to Check in a Supplier’s Test Data
A quick glance at a supplier's test data often reveals whether the report was generated specifically for your shipment or pulled from a generic file. Check that the batch or lot number, material grade, and production date on the test report match the labels on the actual delivered goods. Many discrepancies hide here: a certificate may list a test date months before the supposed production run, or the heat number may belong to a different alloy than what was ordered. If the traceability chain breaks at this first step, every subsequent number on the page loses its meaning.
Pay close attention to the test conditions and methods rather than just the pass/fail conclusion. A tensile test performed at a slower strain rate or with a non-standard specimen geometry can produce values that look acceptable but do not reflect the material's behavior under your application's realities. Compare the reported parameters against the relevant industry standard or the agreed specification, including things like specimen orientation, surface preparation, and ambient temperature. Also ask for the raw measurement data along with the calculated average and standard deviation, because a single averaged value can mask an unstable process or a bimodal distribution that would otherwise raise a red flag.
Look for signs of unusual uniformity or conveniently missing outliers. Real manufacturing and testing always carry some level of variation, so if every reported hardness reading or elongation value sits almost exactly at the nominal target with no scatter, the data may have been smoothed or selectively filtered. Request the calibration records for the test equipment and the operator's qualification details for the specific method used. A legitimate test dataset should include occasional minor deviations, and the supplier should be able to explain them rather than pretend they do not exist.
Sizing, Tolerances, and Custom Fabrication Pitfalls
Getting sizing right on custom parts often feels like a game of telephone between the design team and the shop floor. A dimension that looks fine on a CAD model can turn into an interference nightmare once the part actually gets bent, welded, or anodized. The real trouble usually starts when someone assumes a "standard" clearance will still work after the material is formed or finished. For sheet metal, even a 0.5 mm shift from bend deduction errors can stack up fast across multiple flanges, leaving you with holes that no longer line up and brackets that fight for space.
Tolerances are where the handshake between design and manufacturing either holds firm or falls apart. Designers tend to apply ±0.05 mm everywhere without thinking about process capability, while machinists often quote looser numbers that won’t spoil the fit. The pragmatic middle ground is to assign tight tolerances only where the function truly depends on them, and let the rest ride at a relaxed commercial tolerance. Otherwise you pay a premium for precision that does nothing but inflate cost and lead time, and you still might end up with a part that needs shims or rework because the datums weren’t agreed on in the first place.
Custom fabrication adds another layer of hidden pitfalls, especially when you mix cutting, forming, welding, and finishing under one roof. Weld distortion alone can pull a supposedly straight tube into a banana, and if the drawing doesn’t spell out the post-weld inspection point, you’ll be arguing about who owns the warp. The best defense is a drawing or 3D model that calls out critical-to-function surfaces, realistic material condition modifiers, and a note about which features are reference only. Skip that, and every batch becomes a negotiation about what "close enough" really means.
A Practical Vendor Checklist for Long-Term Supply
Long-term supply agreements tend to look solid on paper until a single point of failure shows up months later. A practical checklist starts with the financials you don't see in a brochure: overdue payables, debt covenants, and how the vendor handles raw material price swings. Ask for a walk through their contingency plans, not just a summary of them. If they can't explain what happens when their top three suppliers fail at once, that's a red flag.
Visiting a facility once is not enough. Go back unannounced during a different shift. Watch how operators handle rework, whether calibration labels are current, and whether the 'quality first' poster actually matches what's happening on the floor. Talk to the people who do the work, not only the sales team. A vendor with stable, cross-trained staff and low turnover is far more likely to keep quality steady over a five-year contract than one running on overtime and temporary workers.
Finally, a genuinely useful checklist includes the boring legal and operational details. Confirm that the vendor's insurance, certifications, and export licenses won't expire mid-contract. Agree on quarterly review meetings that cover more than price. Set clear thresholds for late deliveries, defect rates, and inventory buffers, then put those numbers into the contract with defined remedies. If the vendor resists documenting these details, assume they're already planning to under-deliver.
FAQ
Glass filled PTFE tubes blend PTFE resin with a percentage of glass fiber, typically 15% or 25%. This addition improves compressive strength, dimensional stability under load, and wear resistance. Standard PTFE is softer and creeps more under pressure. The glass filler reduces cold flow while maintaining most of PTFE's low friction and chemical inertness, though it slightly increases surface roughness and may limit use in some ultra-pure fluid lines.
25% glass filled PTFE tubes work well in hydraulic seals, valve seats, pump housings, and bearing applications where parts face steady compression or abrasive contact. They are also used in chemical processing equipment that needs more rigidity than virgin PTFE can offer. The higher filler content suits wear pads, insulators, and structural liners that must hold shape under mechanical load without sacrificing broad chemical compatibility.
Look for a manufacturer that discloses the exact glass fiber percentage, resin grade, and sintering process. Ask for batch test data on tensile strength, elongation, and specific gravity. A good supplier will offer custom inner and outer diameters, cut lengths, and material certifications. Check whether they use virgin PTFE resin rather than reprocessed material, and confirm they can handle tight tolerances for your wall thickness and ovality requirements.
Focus on compressive strength, deformation under load, tensile strength, and coefficient of thermal expansion. Glass filled PTFE typically raises compressive strength to around 1,000 psi or more at 25% filler, while virgin PTFE stays lower. Continuous service temperature remains similar to virgin PTFE, about 260°C, but creep resistance improves markedly. Also evaluate hardness and wear factor if the tube will face sliding contact.
They handle most corrosive chemicals well, similar to virgin PTFE, because the glass fibers are encapsulated within the fluoropolymer matrix. However, strong hydrofluoric acid or hot concentrated alkalis can attack glass fibers over time. For high pressure, the improved creep resistance helps maintain seal integrity and dimensional stability, but pressure ratings depend on wall thickness, temperature, and fitting type, so request rated values from the manufacturer.
A quality supplier can hold outer diameter tolerances within ±0.05 mm for small to medium tubes and wall thickness variation under ±0.1 mm depending on size. Straightness and ovality should be specified, especially for long lengths. Extruded glass filled PTFE tubes often have slightly looser tolerances than machined or molded parts, so ask for a tolerance chart and request first article inspection for critical dimensions.
Higher glass content, such as 25%, improves wear resistance and reduces creep more than 15% glass filled tubes. The fibers create a harder surface that resists abrasive wear and distributes load better. However, higher filler also increases friction against soft mating surfaces and can reduce elongation at break. For dynamic seals or bearings, 25% is common; for less demanding structural parts, 15% may offer a better balance of flexibility and cost.
Conclusion
Glass-filled PTFE tube isn’t just standard PTFE with a pinch of additive; the glass fibers sit throughout the wall, stiffening the structure and giving it far better resistance to cold flow under load. That’s why the material outperforms unfilled PTFE in sealing and bearing applications where dimensional stability matters, yet it stays gentler on mating surfaces than carbon-filled grades, which tend to be more abrasive and electrically conductive. In chemical processing, these tubes hold up against aggressive media while handling higher compressive loads than virgin PTFE, and in high-load, low-speed bearing setups they reduce the risk of creep without sacrificing the low friction PTFE is known for. The real decision point comes down to what you’re sacrificing: if you can tolerate slightly less chemical inertness, you gain a huge jump in wear life and load capacity.
When comparing suppliers, go beyond the polished brochure. Ask for actual test data showing glass content percentage (usually 15% or 25%), tensile strength, elongation at break, and wear rate under your expected pressure and speed. Watch out for sizing drift because glass-filled PTFE expands and contracts differently than virgin material, especially in thin walls or long lengths. Custom fabrication often fails at the tolerance stage—too tight an ID tolerance and the tube can crack during installation; too loose and it leaks. A solid vendor should provide full dimensional reports, batch traceability, and a clear explanation of how they control ovality and wall variation. For long-term supply, check whether they stock multiple rod sizes, offer cut-to-length without delamination, and can handle re-machining if your design shifts. Price matters, but consistency in glass distribution and dimensional control matters more.
Contact Us
Contact Person: Tommy Xiao
Email: [email protected]
Tel/WhatsApp: 8615651509888
Website: https://www.ptfe-factory.com