China Fish Food Making Machine: A Complete Guide for Aquaculture Farmers
2026-10-28
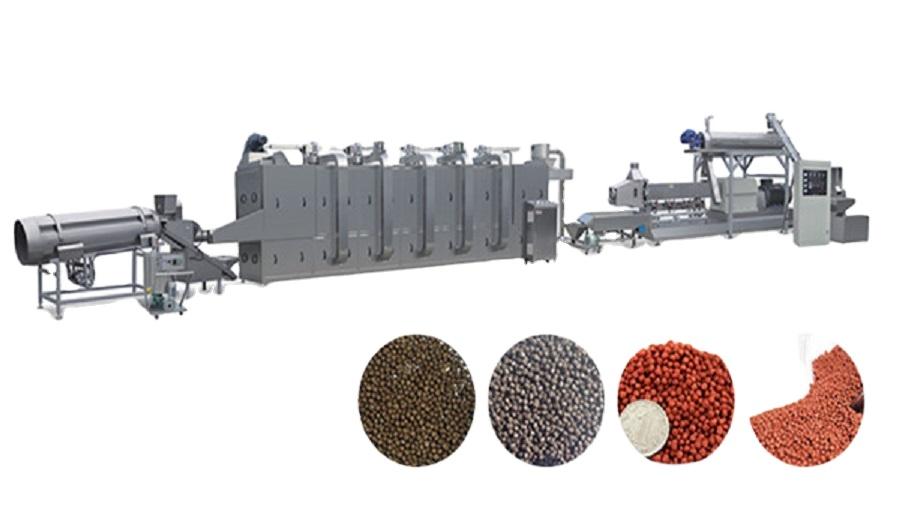
If you’ve ever scooped out undercooked pellets or watched your fish ignore a new batch, you already know why machine choice matters. This guide to China’s fish food making machines goes beyond spec sheets to show how extrusion pressure, die design, and drying time affect real feed conversion. We’ve compared the workhorses and the hype—including why MINGDE has become a name worth checking for farmers who want consistency without paying import premiums.
What a Fish Feed Machine Actually Does on a Chinese Aquafarm
On a typical Chinese aquafarm, a fish feed machine is far more than a simple dispenser. It sits at the edge of a pond or on a floating platform, loaded with a day's worth of pellets, and runs on an adjustable timer that suits the feeding rhythm of species like grass carp or tilapia. The operator sets the interval—often four to six times a day during summer—and the machine flings feed in a wide arc, ensuring even coverage across the water surface. This prevents the aggressive clustering that happens with hand-throwing, where larger fish monopolize the food and smaller ones starve.
The real value shows up in how the machine adapts to pond conditions. In ponds with strong aeration or wind-driven currents, the feed needs to land closer to the bank or in sheltered corners, and a decent machine lets you angle the discharge chute or change the throwing distance. Many farmers also mix different pellet sizes in the hopper—fine powder for fry, larger sinking pellets for bottom feeders—and the machine's agitator keeps the mix from clogging. Over time, farmers learn the exact settings that reduce uneaten feed sinking to the bottom, which otherwise fuels algae blooms and raises ammonia levels.
Maintenance is a daily ritual rather than a technical headache. After the last feeding, the hopper gets brushed clean to prevent pellet dust from caking in humid weather, and the throwing plate or spinner is checked for wear. Some older machines run on a simple mechanical clock, while newer ones have a small keypad, but the principle stays the same: let the machine handle the repetitive tossing while the farmer spends his time checking water color, repairing nets, or sorting fish for market. It is not about automation for its own sake; it is about freeing up hands during the busiest months of the growing season.
Matching Machine Capacity to Your Daily Feeding Routine
Choosing the right machine capacity starts with how much your pet actually eats in a day, not the largest hopper you can find. A feeder that holds two weeks of kibble might sound convenient, but if your cat only gets a third of a cup twice daily, that food sits for a long time and loses its crunch. Smaller hoppers force more frequent refills, which keeps meals fresher and lets you spot changes in appetite sooner.
A practical way to match capacity is to multiply your pet's daily portion by the number of days you want between refills—usually five to seven is a comfortable window. If your dog eats two cups a day, look for a hopper that holds around ten to fourteen cups, with a little extra room for the dispensing mechanism. That way you're not topping off every other day, but you're also not letting food go stale in a half-empty bin.
For multi-pet homes or routines that shift on weekends, adjustable portion settings matter more than raw hopper size. You can dial in different meal amounts for morning and evening, and the machine's capacity simply needs to cover the busiest day of the week. If you do opt for a larger hopper, toss in a food-safe desiccant pack and clean the bin between full cycles—otherwise a bigger capacity just becomes a bigger stale-food trap.
Raw Ingredients That Work Best in Local Extruders
Local extruders tend to reward consistency over exotic material choices. Uniform pellet size, low moisture content, and a melt flow index suited to the screw design matter more than the base polymer's brand name. If the feedstock varies too much from batch to batch, operators spend more time adjusting barrel temperatures than actually producing anything.
Recycled polypropylene and high-density polyethylene are often the most forgiving starting points. They tolerate occasional contamination better than brittle resins and can be blended with a small percentage of virgin material to stabilize output. Avoid heavily filled compounds unless the extruder has hardened screws and barrels; abrasive fillers wear down local equipment quickly.
Some of the best results come from mixing locally available regrind with a slip agent or a processing aid. This not only reduces viscosity but also helps prevent bridging in the hopper. Keep an eye on fines and dust—they tend to separate during conveying and create inconsistent feed, especially in smaller extruders without force-feeding.
Maintenance Habits That Keep Production Steady
Most line stoppages don't come from dramatic equipment failures. They come from skipped inspections, worn parts nobody noticed, and schedules that drift until a small issue becomes a full shift lost. The teams with the steadiest output treat maintenance less like a repair task and more like a daily rhythm—checking the same critical points at the same times, logging what they see, and acting on the first sign of drift instead of waiting for a fault light.
One habit that consistently pays off is the ten-minute walkthrough at shift change. The outgoing operator and the incoming one both look at the key gauges, listen for changes in motor pitch, and feel for heat or vibration that wasn't there yesterday. It sounds simple, but it catches most developing problems early enough to fix during scheduled downtime—not during a production run. Another is keeping spare parts for the top five failure points always in stock, with a clear reorder trigger when inventory drops below two weeks of use.
The real difference shows up in how teams handle small anomalies. A slight increase in cycle time, a new squeak on a conveyor, a filter that clogs a day earlier than usual—these are treated as data, not annoyances. When operators and maintenance staff share the same log and the same morning huddle, fixes happen before the line ever stops. Production stays steady not because nothing ever breaks, but because the plant is always one step ahead of the breakdown.
Comparing Pellet Sizes and Shapes for Different Fish Species
Not all fish pellets are created equal, and the difference starts with size. A tiny neon tetra can’t handle the same pellet a full-grown cichlid crushes in seconds. Manufacturers often scale pellet diameters from micro granules under 0.5 mm for fry and small community fish up to 6 mm or more for large predators. But it’s not just about mouth gape—feeding behavior matters too. Surface feeders like hatchetfish do best with floating micro pellets that stay suspended, while bottom dwellers such as corydoras need sinking wafers or discs they can rasp at on the substrate. Getting the size wrong leads to wasted food, poor growth, and fouled water.
Shape plays a surprisingly nuanced role in how different species accept pellets. Round spheres roll away from slow grazers like goldfish, so flattened discs or crumbled chunks give them a better chance to nibble. For mid-water hunters such as bettas, tiny slow-sinking granules mimic the movement of small prey and trigger a feeding response. Some marine herbivores, like tangs, prefer thin sheets or flakes pressed into pellet form that they can scrape against rocks. There’s no universal “best” shape—only the one that matches the fish’s natural foraging style. Try observing how a new species approaches food before committing to a bulk purchase.
Matching pellet size and shape to the fish isn’t a one-time task. Juveniles grow fast, and their food needs to grow with them. A swordtail fry that starts on powder may need crumble within weeks, then small granules by month three. Likewise, a shy nocturnal catfish might ignore hard round pellets but eagerly vacuum soft, irregularly shaped sinking morsels. Keep a few different pellet types on hand and watch which ones disappear fastest. The best pellet is the one your fish actually eat without hesitation—everything else is just marketing.
Budgeting for a Fish Feed Line Without Overpaying
Start by auditing your actual production needs. Many operators overspend by choosing a line rated far above their weekly output, only to discover the extra capacity sits idle while energy bills climb. Map out realistic batch sizes and shift patterns first, then match equipment to that data rather than to a sales pitch.
Consider rebuilt or refurbished extruders and dryers from reputable suppliers. A well-maintained used line can deliver 80% of the performance of a new one at half the upfront cost. But insist on a detailed service history and test run before committing. Also factor in spare parts availability—a cheap machine that forces you to import a $200 impeller every month is no bargain.
Don't let the initial quote be the final word. Ask about phased payment terms, off-season discounts, or bundling installation and training. Many manufacturers will trim 5–10% if you can accept a longer lead time or a floor model. And remember to budget for the unglamorous stuff: electrical upgrades, screw conveyors, and dust collection—these often surprise first-time buyers and blow the budget faster than the headline equipment.
FAQ
Look beyond the motor power and price. Inspect the die plate thickness, the quality of the bearing housing, and whether the supplier offers a local spare parts list. Ask for a video of the machine running your specific feed formulation, not just a demo with pre-mixed soybean meal. Also confirm the voltage and frequency match your farm's power supply, and clarify the shipping terms for heavy components.
Base it on the daily feed requirement at peak season, not on the total pond area. For a farm producing 200 to 500 kilograms of pellets per day, a 90 to 132 model with a 7.5 kW motor usually works. If you mix your own wet ingredients often, pick a model with a slightly larger die opening and a heavier gearbox to handle the extra load without overheating.
Soybean meal, rice bran, fishmeal, corn gluten, and cassava starch all extrude well, but you need to keep moisture between 18 and 22 percent. Freshwater fish diets often include 10 to 15 percent peanut meal, which can clog smaller dies if not finely ground. Avoid adding too much raw starch at once; pre-gelatinize it with hot water or steam for better binding.
That usually means the compression temperature is too low or the material stayed in the barrel too briefly. Check whether the screw or roller clearance has worn beyond tolerance. Also look at the moisture distribution: wet clumps pass through unevenly. Add a little vegetable oil or a natural binder like wheat flour at 3 to 5 percent and run the machine at full load for ten minutes before collecting finished pellets.
Clean the die holes after every batch while the barrel is still warm, using a soft brass brush instead of steel. Grease the main bearings every 40 operating hours and check the belt tension weekly. If you hear a metallic knocking sound, stop immediately and inspect the roller assembly. Keep a spare die, a set of rollers, and two drive belts in stock because shipping replacements from China can take three to six weeks.
Usually yes, but only after you pass the break-even volume. For example, if commercial floating catfish feed costs 650 to 750 dollars per ton locally, making your own with soybean meal, maize, and fishmeal can bring the cost down to 420 to 500 dollars per ton, even after electricity and labor. The savings grow if you have at least 20 tons of annual feed demand. Smaller farms may not recover the machine cost quickly unless they share it with neighbors.
The biggest one is changing the moisture level too fast. Dump dry meal into a hot barrel and the product will jam or produce brittle pellets. Another mistake is running the machine at full speed before it warms up, which shortens the screw life. Also, many operators ignore the cooling step and stack warm pellets in bags, causing mold within a week. Let pellets cool to room temperature and dry in a shaded, well-ventilated area.
Conclusion
On a Chinese aquafarm, a fish feed machine transforms raw grains and proteins into uniform pellets that sink or float depending on die settings and moisture. Instead of buying commercial feed, farmers can grind local ingredients like soybean meal, rice bran, fishmeal, and cassava, then extrude them under heat and pressure. The result is a dense, digestible pellet that cuts waste and lets you adjust recipes as fish grow. Matching machine capacity to your daily feeding routine matters more than chasing the highest horsepower. A small pond operation might run a 100–150 kg per hour extruder for a couple of hours each morning, while a multi-pond setup needs something that can finish the day's ration without running all night. Raw ingredients that work best in local extruders are usually dry, finely milled, and low in fiber. Too much moisture or coarse grain causes clogging and uneven expansion.
Maintenance habits keep production steady. After every batch, clear the die holes and check the cutter blades; a quick oiling of bearings and a weekly belt tension check prevent the kind of sudden breakdown that leaves fish unfed. Pellet size and shape are not one-size-fits-all. Carp and tilapia do well on 2–4 mm sinking pellets, while catfish often prefer larger, harder pellets that hold together in warm water; floating pellets for herbivorous species need higher starch content to expand properly. Budgeting for a fish feed line without overpaying means starting with a basic dry-type extruder if your volume is under one ton per day, then adding a mixer and dryer only when output justifies it. Many Chinese suppliers bundle unnecessary accessories, so focus on motor quality, screw material, and spare parts availability rather than cosmetic features. A well-chosen machine paired with consistent maintenance usually pays for itself within the first year through reduced feed costs.
Contact Us
Contact Person: LILY SUN
Email: [email protected]
Tel/WhatsApp: 0086-13969103791
Website: https://www.snackfoodmachinery.com/